How to Cut, Drill and Bend PVC Foam Board: A Complete Fabrication Guide
PVC foam board machines like wood, but it is not wood. It is a thermoplastic. Push a saw through it too fast and the cut edge melts and re-welds behind the blade. Drill it without the right feed and the bit grabs. Bend it cold and it cracks instead of curving.
This guide covers the six fabrication processes you will actually use — sawing, drilling, routing, grooving, thermoforming and finishing — with the settings and failure modes that matter. It is written for cabinet makers, signage fabricators and interior fit-out workshops working with Celuka (density 0.4–1.0 g/cm³), free foam (0.3–0.35 g/cm³), WPC (5–30 mm) and co-extrusion board.
What you are cutting
Three things about the material determine every setting in this guide:
|
Property |
Why it changes your settings |
|
Thermoplastic |
Friction heat softens the material. Speed and feed must stay in balance or the kerf closes behind the tool |
|
Foamed core |
The core is less dense than the skin. The same blade behaves differently on a Celuka skin than on a free-foam core |
|
Calcium content rises with density |
A 0.7–1.0 g/cm³ board wears tooling faster than wood of the same thickness |
One practical consequence: if you are using a board that has been stored in a cold container or cold warehouse, let it acclimatise for at least 24 hours before machining. Cold board is more brittle and more likely to chip on the edges.
1. Sawing
Tooling: fine-tooth carbide blades. Carbide holds an edge against the calcium filler; fine teeth reduce chipping on the skin.
The setting that matters most: spindle speed. PVC melts at the cut if the blade runs too fast for the feed rate. The practical rule is to lower the spindle speed and keep the feed rate steady, rather than running fast and slow-feeding.
|
Operation |
What to watch |
|
Panel saw / table saw |
Fine-tooth carbide; steady, moderate feed; support the offcut — unsupported sheets pinch the blade |
|
Circular saw |
Reduce spindle speed; avoid dwelling in one spot |
|
Band saw |
Good for curves and thick sections; clear the swarf |
|
Hand saw |
Workable for small cuts; fine tooth, light pressure |
Failure modes: melted and re-welded kerf (speed too high), chipped edges (dull blade or excessive feed), bowed cut (unsupported sheet).
2. Drilling and screwing
Drilling: standard HSS or carbide-tipped bits work. Use a moderate speed with a firm, steady feed — too slow and the material smears, too fast and it melts. Back the panel with a sacrificial board to prevent blow-out on the exit side, and clear chips from the flutes frequently.
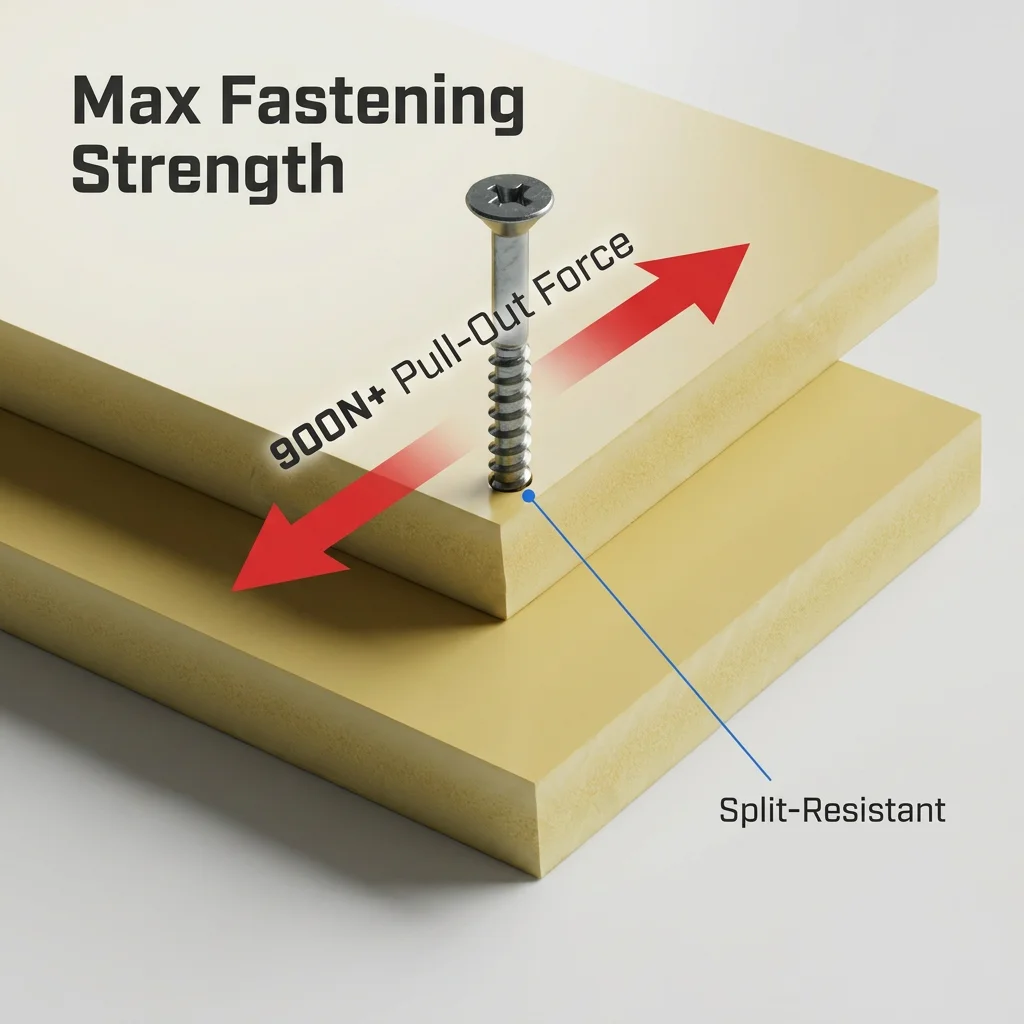
Screwing: the result depends almost entirely on density, not on technique.
|
Board |
Recommended density for screw-holding |
Guidance |
|
Celuka (PL-01) |
0.5–0.7 g/cm³ high range |
Best balance of strength and weight for hardware fixing |
|
WPC (PL-03) |
0.5–0.7 g/cm³ |
Higher screw-holding than standard PVC foam because of the wood/bamboo fibre |
|
Co-extrusion (PL-04) |
0.5–0.85 g/cm³ |
Dedicated hard surface layer gives the best screw retention |
|
Extra-high density (PL-01 0.7–1.0 g/cm³) |
— |
Use where load demands it, but expect faster tooling wear |
|
Free foam (PL-08) |
0.3–0.35 g/cm³ |
Not intended for load-bearing or hardware fixing |
Pre-drill when you are close to an edge, and avoid over-tightening — PVC will strip a thread more readily than hardwood.
3. CNC routing and engraving
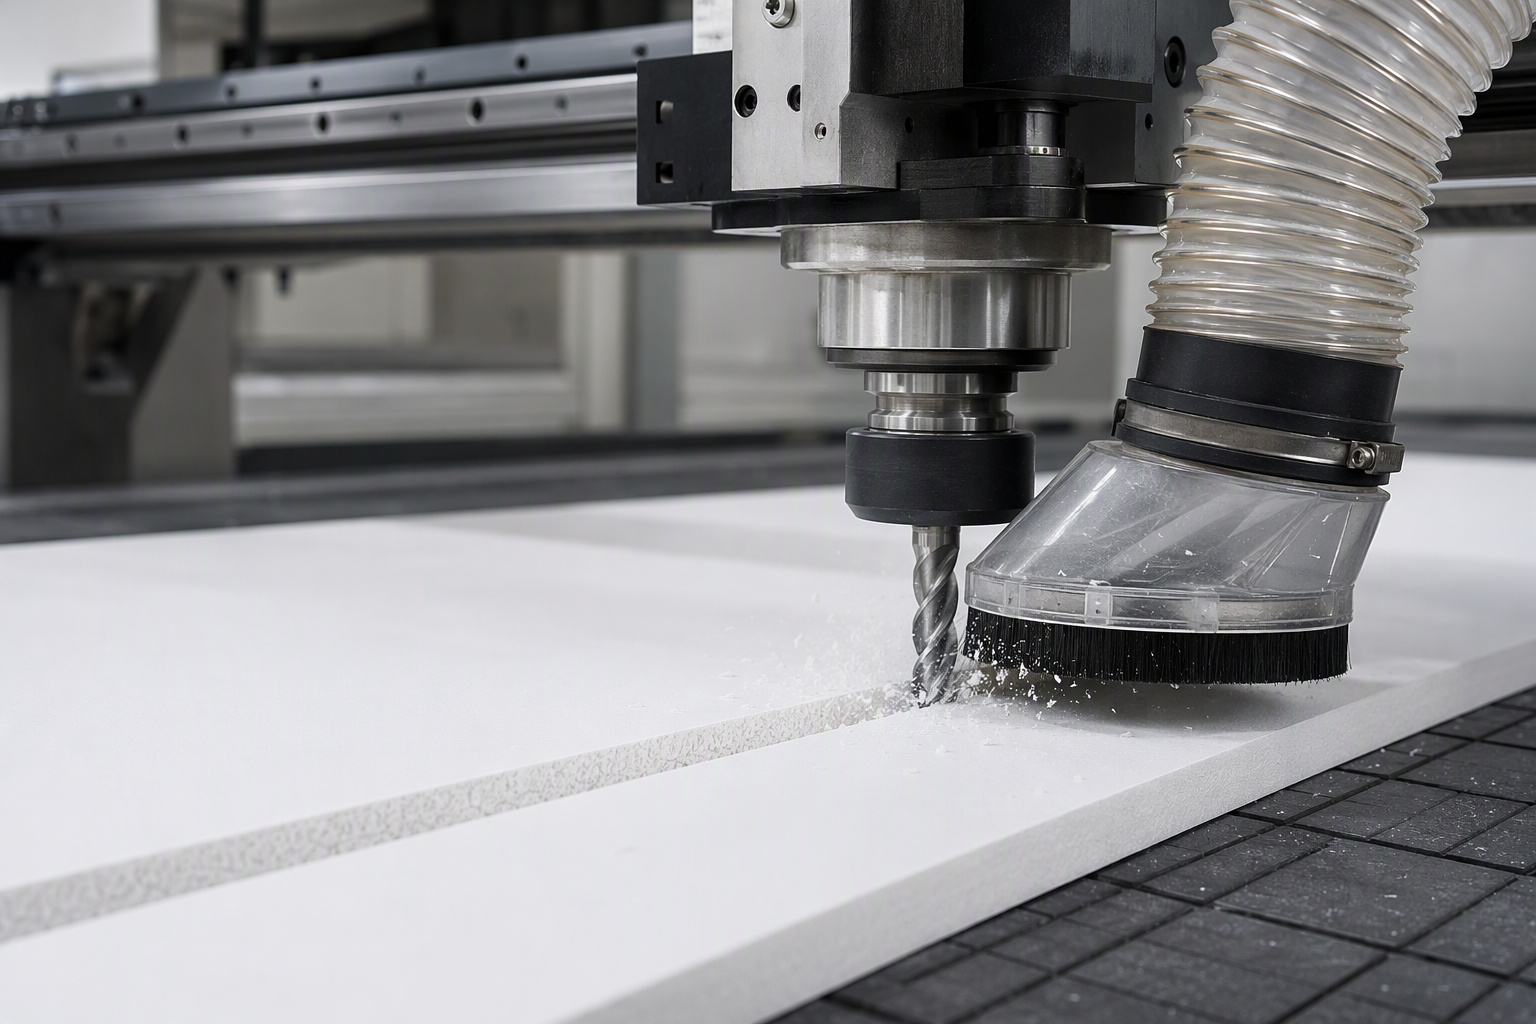
This is where PVC foam board performs best, and where the parameters matter most.
Bits: single-flute or double-flute spiral bits. Single flute gives better chip clearance on softer, lower-density board; double flute gives a cleaner edge on higher-density and laminated material.
Spindle speed: reduce compared with wood. High RPM plus a slow feed is the classic recipe for a gummy, welded edge.
Feed rate: steady and reasonably brisk. The chip should be a clean shaving, not dust and not a smear.
Depth of cut: take multiple moderate passes rather than one deep pass on thick stock.
Dust extraction: essential. PVC chips are static-prone and will cling to the machine, the bed and the finished surface.
Engraving: coloured co-extrusion board (3 core colours plus 9 surface colours) and coloured Celuka produce a two-tone effect when engraved — the surface layer is cut through to reveal the contrasting core. No lamination or painting is needed to get a coloured carved look. That is the single most useful property of co-extrusion board for signage work.
4. Grooving, 45° mitring and edge banding
Grooving works on Celuka and co-extrusion board; the dense skin holds the groove profile. Lower-density free foam does not hold a groove reliably.
45° mitring is standard for cabinet door edges and box sections. Use a fine-tooth blade, support both pieces, and clamp rather than rely on friction when assembling.
Edge banding covers the exposed core. Our PL-07 edge banding is available in 1×19 mm, 1×22 mm and 1.2×22 mm, with other sizes on request, and is designed to match PL-02 laminated boards. Standard EVA hot-melt edge banders work; PUR hot melt gives a stronger, more moisture-resistant bond.
5. Thermoforming and bending
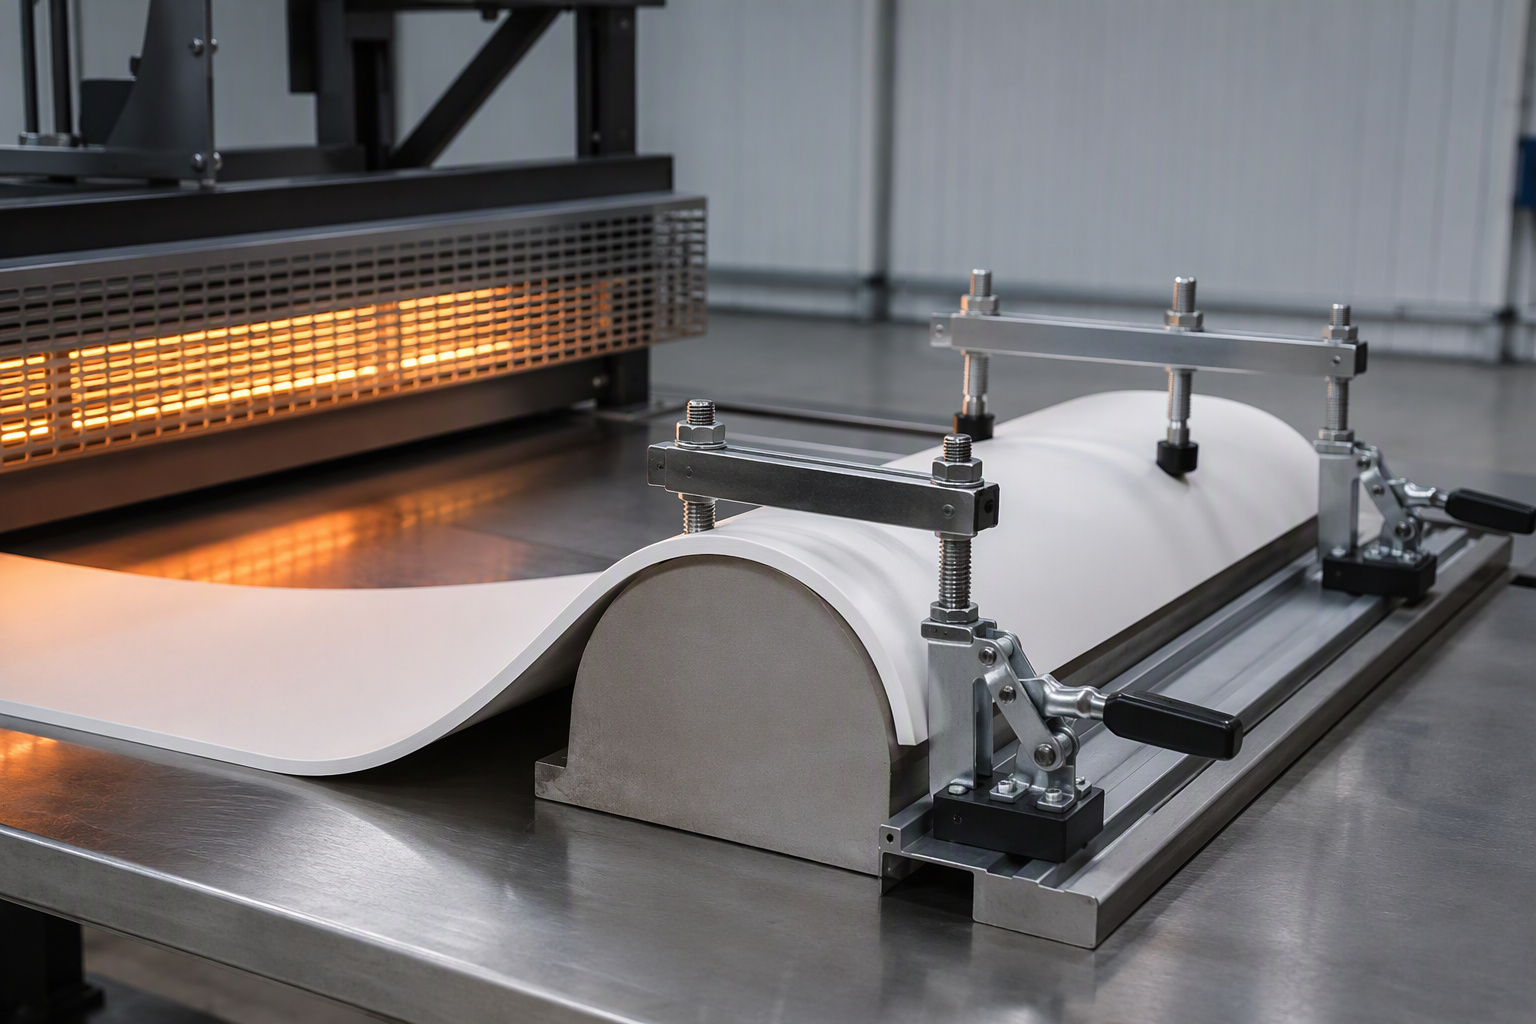
PVC foam board can be heat-formed into curves and simple shapes.
Heat range: approximately 100–140 °C
Method: even heat on both sides, then form over a jig or former while the sheet is still pliable
Radius: keep the radius generous — tight radii on thick, high-density board will stress-crack
Cooling: let the part cool in the jig. PVC holds the formed shape as it cools
Cold bending is possible only for very gentle curves on thin, low-density sheet. For anything structural, use heat.
Note that we do not currently publish a formal fabrication guide with recommended bend radii by thickness, and our technical team is happy to advise case by case.
6. Painting, printing and laminating
Painting: Celuka (PL-01) and WPC (PL-03) boards accept spray painting after sanding and priming with a PVC-specific primer or PU paint. Laminated (PL-02), marble UV (PL-05) and wall panel (PL-06) products are pre-finished, so painting is not recommended on those.
UV printing and screen printing: both work well on flat, white Celuka and free-foam surfaces. Free foam in 3–10 mm is the usual choice for printed advertising boards; Celuka in 5–10 mm is used where the printed panel also needs rigidity and a longer service life.
Laminating: we run an in-house lamination workshop staffed by 12 people, using PUR hot melt. If you buy board and laminate it yourself, PUR hot melt is the adhesive class used on our own line.
Adhesive selection by application:
|
Bonding |
Recommended adhesive |
|
Board to board |
PVC solvent cement or structural adhesive |
|
Wall mounting |
Nail-free adhesive / MS polymer |
|
Lamination |
PUR hot melt |
|
Edge banding |
EVA or PUR hot melt |
|
To metal or glass |
MS polymer or structural adhesive |
The six mistakes that ruin a cut
Spindle speed too high. Melted edges, welded kerf, burned smell. Lower the RPM.
Feed rate too slow for the RPM. Same result, different cause — the tool dwells and friction builds.
No dust extraction. Static-charged chips pack the cut and scratch the finished surface.
Unsupported sheet. Offcut sags, pinches the blade, and produces a bowed cut.
Wrong density for the job. Grooving or screwing a 0.3–0.35 g/cm³ free-foam board will not hold — that is a material selection error, not a machining error.
Cutting cold board. Brittle edges and chips. Let it acclimatise for 24 hours.
Quick reference
|
Process |
Tooling |
Key setting |
Works on |
|
Sawing |
Fine-tooth carbide |
Reduced spindle speed, steady feed |
All densities |
|
Drilling |
HSS / carbide-tipped |
Moderate speed, firm feed, backer board |
All densities |
|
Screwing |
— |
Density 0.5–0.7 g/cm³ recommended |
Celuka, WPC, co-extrusion |
|
CNC routing |
Single/double-flute spiral |
Lower RPM than wood, brisk feed, extraction |
All densities |
|
Engraving |
Spiral or V-bit |
Multiple passes |
Celuka, co-extrusion (coloured) |
|
Grooving |
Fine-tooth or router |
— |
Celuka, co-extrusion |
|
Thermoforming |
Heat 100–140 °C + jig |
Even heat, generous radius |
All densities |
|
Edge banding |
EVA / PUR hot-melt bander |
Match PL-07 to PL-02 |
Celuka, WPC, co-extrusion, laminated |
Frequently asked questions
Can PVC foam board be cut on a standard table saw?
Yes. Use a fine-tooth carbide blade and reduce the spindle speed compared with wood. The main risk is frictional heat melting the cut edge, which is managed by keeping the feed rate steady rather than slowing it down.
What density do I need for screws and hardware?
0.5–0.7 g/cm³ is the most commonly used range for cabinet carcasses, doors and hardware-mounting areas. High-density Celuka at 0.55–0.75 g/cm³ is recommended where loads are heavier. Free foam at 0.3–0.35 g/cm³ is not intended for hardware fixing.
At what temperature does PVC foam board bend?
Approximately 100–140 °C, applied evenly to both sides, then formed over a jig and left to cool in place.
Does the board need special tools?
No special tooling is required — standard woodworking equipment (table saw, CNC router, edge bander, drill) works. Extra-high-density board at 0.7–1.0 g/cm³ does wear tooling faster than wood.
Can engraved board give a coloured effect without painting?
Yes, if you start with coloured co-extrusion board or coloured Celuka. Cutting through the surface layer exposes the contrasting core colour, so no lamination or painting is needed.
Talk to our technical team
We manufacture Celuka, free foam, co-extrusion, WPC, laminated, marble UV and wall panel products, so we can recommend the right board for your process rather than the other way around. Send us your equipment and the application, and our team will advise on density, thickness and expected behaviour.
Hangzhou Jiaying Trade Co., Ltd. (Pluswin) — PVC and WPC board manufacturer in Hangzhou, Zhejiang, China, established 2006. 13 active certifications issued by SGS, Intertek and FEMKO.
Recommended Products

Hot News
-
How to Cut, Drill and Bend PVC Foam Board: A Complete Fabrication Guide
2026-09-24
-
PVC & WPC Foam Board FAQ
2026-09-24
-
PVC Foam Board & WPC Board FAQ: Products, Customization, Quality and Shipping
2026-09-08
-
How to Test the Quality of PVC Foam Board: A Practical Buyer’s Guide
2026-09-08
-
Luxury Without the Price Tag: How PVC Marble Sheets Are Redefining Modern Interior Aesthetics
2026-08-14
-
Discover the rigorous quality control process inside the PLUSWIN factory. Learn how we guarantee consistent thickness, zero formaldehyde, and superior durability in every PVC board batch
2026-07-21
-
CustomSize PVC Foam Boards from Professional Manufacturer JIAYING PLUSWIN
2026-06-05
-
Product Advantages of Hangzhou Jiaying Trade Co., Ltd.
2026-03-27
-
Recommended PVC Board Manufacturers in China: Dual Assurance of Quality and Service
2026-01-23
-
Fewer Layers, Greater Intelligence: How 3-Layer PVC Co-Extruded Boards Deliver Superior Performance
2025-12-11